Expansion Joint Suppliers & Manufacturers In Malaysia: Diagnosing Expansion Joint Equipment Failures

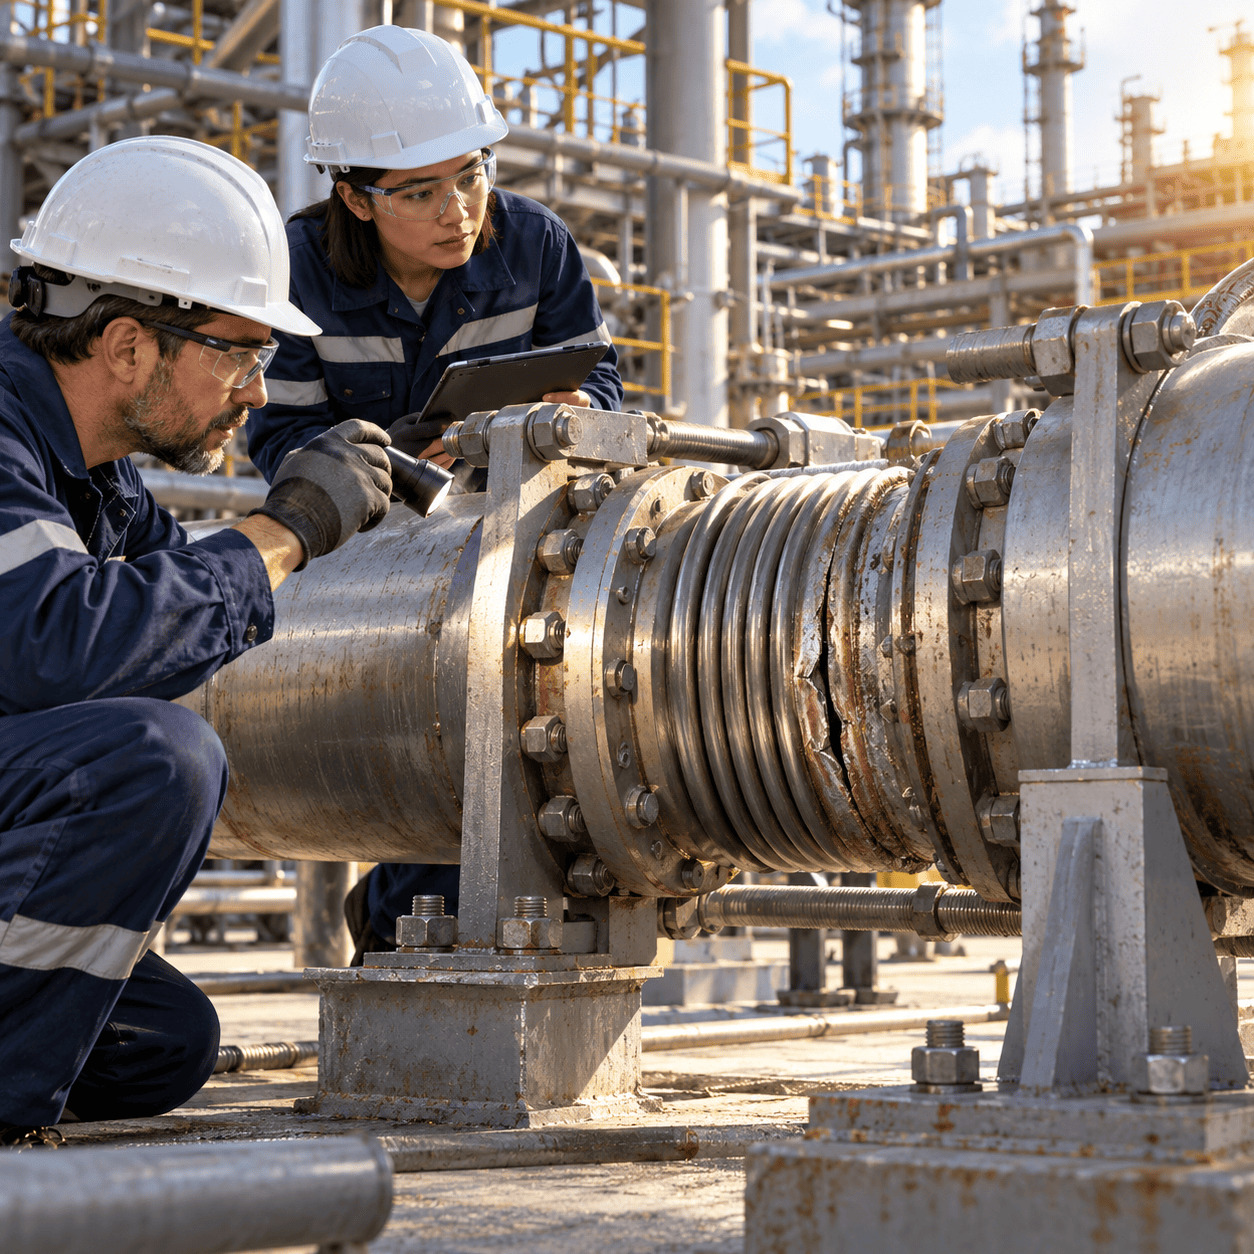
A failed expansion joint rarely tells the full story at first glance. A crack may resemble fatigue, but the initiating condition could be corrosion thinning, excessive lateral displacement, pressure instability, vibration, or an installation problem. For plant engineers, reliability teams, inspectors, and turnaround personnel, the challenge is to separate visible damage from the system condition that created it.
Replacing a failed bellows without identifying the root cause can allow the same failure to recur. A proper investigation should consider operating history, movement demand, pressure and temperature transients, process media, anchors, guides, supports, and any piping modifications.
This is also where an experienced expansion joint supplier in Malaysia can add value. Rather than assessing only the damaged component, the review should consider how the joint has interacted with the wider piping system throughout its service life.
Start With The Original Design Basis
Failure analysis should begin by comparing the original design basis with actual field conditions. Key information may include operating pressure, temperature, required axial, lateral and angular movement, cycle count, process medium, bellows material, spring rate, effective area, restraint arrangement, and installation geometry.
The surrounding piping system should also be examined. Bellows are intentionally flexible, which means problems elsewhere in the line can become concentrated at the joint. A displaced anchor, seized guide, settling support, equipment nozzle movement, or piping modification can significantly change the movement imposed on the bellows.
Where original calculations or drawings are unavailable, field measurements become particularly important. Face-to-face dimensions, convolution condition, flange alignment, tie-rod position, and piping offset can help engineers reconstruct what the system has experienced during service.
Fatigue And Corrosion In Expansion Joint Equipment
Fatigue develops through repeated cyclic strain. In metal bellows, cracking often initiates at highly stressed areas of the convolution and propagates as movement cycles accumulate.
The key question is not simply whether pressure and temperature remain within their stated limits. Bellows also have a finite movement cycle life.
Startups, shutdowns, thermal transients, vibration, and operating changes may expose a joint to more cycles than originally anticipated. Combined movements also matter. A joint intended primarily for axial movement may experience lateral displacement because of support movement or field misalignment, increasing local stress and potentially reducing fatigue life.
Corrosion can complicate diagnosis. Pitting, wall thinning, stress corrosion cracking, or erosion may weaken the material before cyclic stresses produce the final crack.
For this reason, expansion joint manufacturers in Malaysia may need to consider both process-side conditions and the external operating environment when evaluating a premature failure.
Chloride contamination, wet insulation, marine exposure, condensate, chemical cleaning residues, and deposits around convolutions can all contribute. Depending on the failure, further investigation may include thickness measurements, positive material identification, surface NDE, metallography, or laboratory analysis.
Overpressure and Instability In Expansion Joint Equipment
Overpressure does not always cause immediate rupture. Permanent deformation, irregular convolution geometry, bulging, or instability may instead indicate that the joint experienced a transient load beyond its intended design condition.
Possible causes include blocked lines, valve events, pressure surges, abnormal startup conditions, or process upsets.
Pressure thrust must also be considered. An unrestrained bellows develops axial force from internal pressure acting over its effective area. If anchors, tie rods, hinges, or other restraints do not perform as intended, the resulting movement can push the bellows outside its allowable range.
Vacuum and external pressure introduce different risks. Depending on the joint geometry and operating conditions, instability or squirm can occur even when positive-pressure performance appears satisfactory.
For critical expansion joint equipment, failure analysis must consider actual system pressure behaviour rather than focusing only on the component’s stated pressure rating.
Installation Damage Can Resemble Operating Failure
Installation-related damage can closely resemble service-induced failure.
Uneven convolution spacing, permanent lateral offset, dents, torsional deformation, flange mismatch, or abnormal tie-rod positions may indicate issues introduced during transport, fit-up, installation, or commissioning.
A bellows should not be used to pull misaligned piping into position. Doing so consumes part of its available movement capacity before the system reaches operating temperature. Forced alignment can also introduce stresses that were not included in the original design calculation.
Incorrect handling of shipping bars, welding damage, wrong liner orientation, improper presetting, and incorrect removal or adjustment of tie rods may also compromise performance.
A premature failure investigation should therefore review installation history alongside operating data rather than assuming that the bellows itself was defective.
Read The Failure Pattern, Not Just The Crack
Failure morphology must be interpreted alongside the behaviour of the piping system.
A circumferential crack may indicate cyclic bending, but the investigation must still determine what generated that repeated bending. Localised thinning may indicate corrosion, but engineers need to identify the source of the corrosive environment.
Likewise, a deformed bellows may result from pressure instability, excessive compression, lateral displacement, torsion, or loss of restraint.
Anchors, guides, supports, and connected equipment can provide evidence that the failed component alone cannot.
Operating history is equally important. Piping modifications, equipment replacement, throughput increases, process chemistry changes, or altered startup procedures may mean the original design basis no longer reflects the actual service conditions of the expansion joint equipment.
Why “Like-for-Like” Replacement Can Be Misleading
Two bellows can share the same nominal diameter, face-to-face dimension, and material while behaving differently in service.
Convolution geometry, ply arrangement, spring rate, effective area, liner construction, restraint configuration, and movement capacity all affect how loads transfer through the piping system.
That is why reputable expansion joint manufacturers in Malaysia evaluate the current operating duty rather than simply reproducing an old specification.
A stiffer replacement may reduce local movement while increasing loads on equipment nozzles, anchors, or supports. Additional restraints can alter how pressure thrust is transferred through the system. A thicker bellows may appear more robust but can also change flexibility and fatigue behaviour.
The correct replacement is therefore not automatically the strongest component. It is the configuration that appropriately manages movement, pressure, temperature, chemistry, cycling, and piping reactions together.
Spring Rate And System Interaction In Expansion Joint Equipment
Spring rate is often overlooked during replacement projects, yet it can significantly affect piping loads.
A replacement joint with a substantially different axial or lateral spring rate changes the force required to achieve the intended movement. This can alter reactions at anchors, guides, equipment nozzles, or structural supports.
Effective area is equally important because it influences pressure thrust. A replacement joint that appears dimensionally equivalent may still behave differently under pressure if its internal geometry changes.
For critical systems, replacements should therefore be reviewed in relation to piping stress requirements rather than approved solely through dimensional comparison.
Corrective Action Should Address The Failure Mechanism
Once the failure mechanism has been established, corrective action may involve more than changing the bellows material.
Potential changes may include:
- bellows metallurgy
- convolution geometry
- ply configuration
- internal liners
- tie rods or other restraints
- anchors and guides
- insulation or external protection
- movement allocation
- the overall expansion joint arrangement
For critical service, revisions may also need to be coordinated with piping stress, structural, process, and rotating-equipment requirements.
If the original failure originated from an anchor, guide, support, installation issue, or wider system-layout problem, changing the bellows alone will not remove the underlying cause.
The objective should be to determine whether the failure is primarily component-specific or system-driven before finalising the replacement specification.
Documentation Expected From Expansion Joint Manufacturers in Malaysia
For critical-service applications, documentation forms part of the engineering assessment.
Depending on the project and applicable requirements, documentation may include design calculations, approved drawings, material certificates, welding records, welder qualifications, NDE reports, dimensional inspection records, pressure or leak-test documentation, and Certificates of Conformance.
These records allow engineers to verify that the replacement corresponds with the specified duty and provide a useful baseline for future inspection and troubleshooting.
Good documentation also improves traceability. If operating conditions change or another problem occurs later, engineers can compare field performance against the assumptions used to design and manufacture the expansion joint equipment.
What To Expect From A Trusted Supplier
Selecting a supplier for critical-service expansion joints involves more than comparing nominal dimensions, material grades, and pricing.
Technical support should include a review of the application, movement requirements, operating conditions, restraint arrangement, surrounding piping behaviour, and relevant documentation. Where a failure has already occurred, inspection findings and operating history should also inform the replacement strategy.
At Recovered Energy Engineering, we support customers across the lifecycle of metal, fabric, and rubber expansion joints, including design, supply, installation, inspection, troubleshooting, replacement, testing, and commissioning.
If your expansion joints show cracking, leakage, deformation, corrosion, abnormal movement, or repeated premature failure, our team can review operating conditions, assess likely failure mechanisms, examine the surrounding piping system, and help define a replacement approach based on the actual application.
Our experience supporting oil and gas, petrochemical, power, marine, and industrial facilities provides practical insight into shutdown requirements, field constraints, critical piping systems, and lifecycle reliability.
If you are looking for an experienced, reputable expansion joint supplier in Malaysia, contact Recovered Energy Engineering to discuss the application before proceeding with another like-for-like replacement.